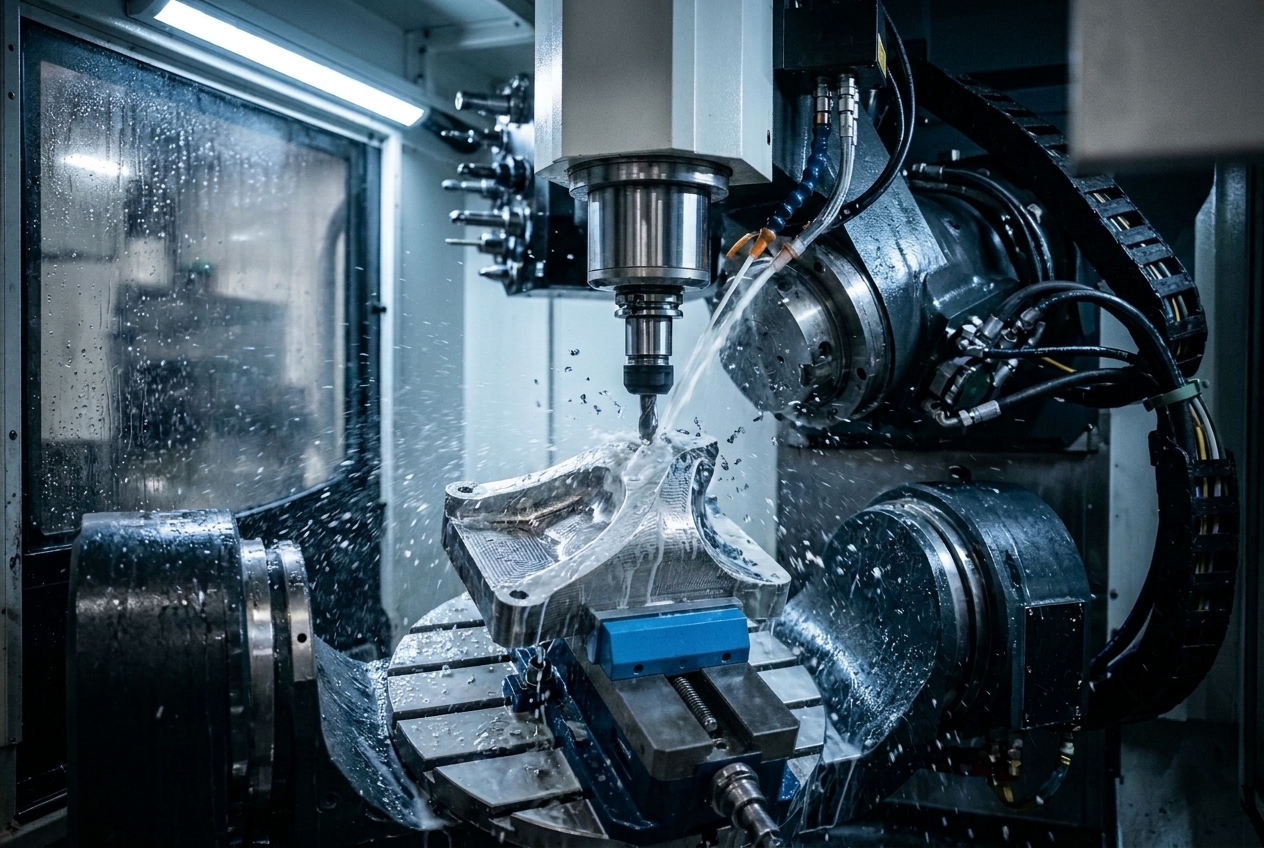
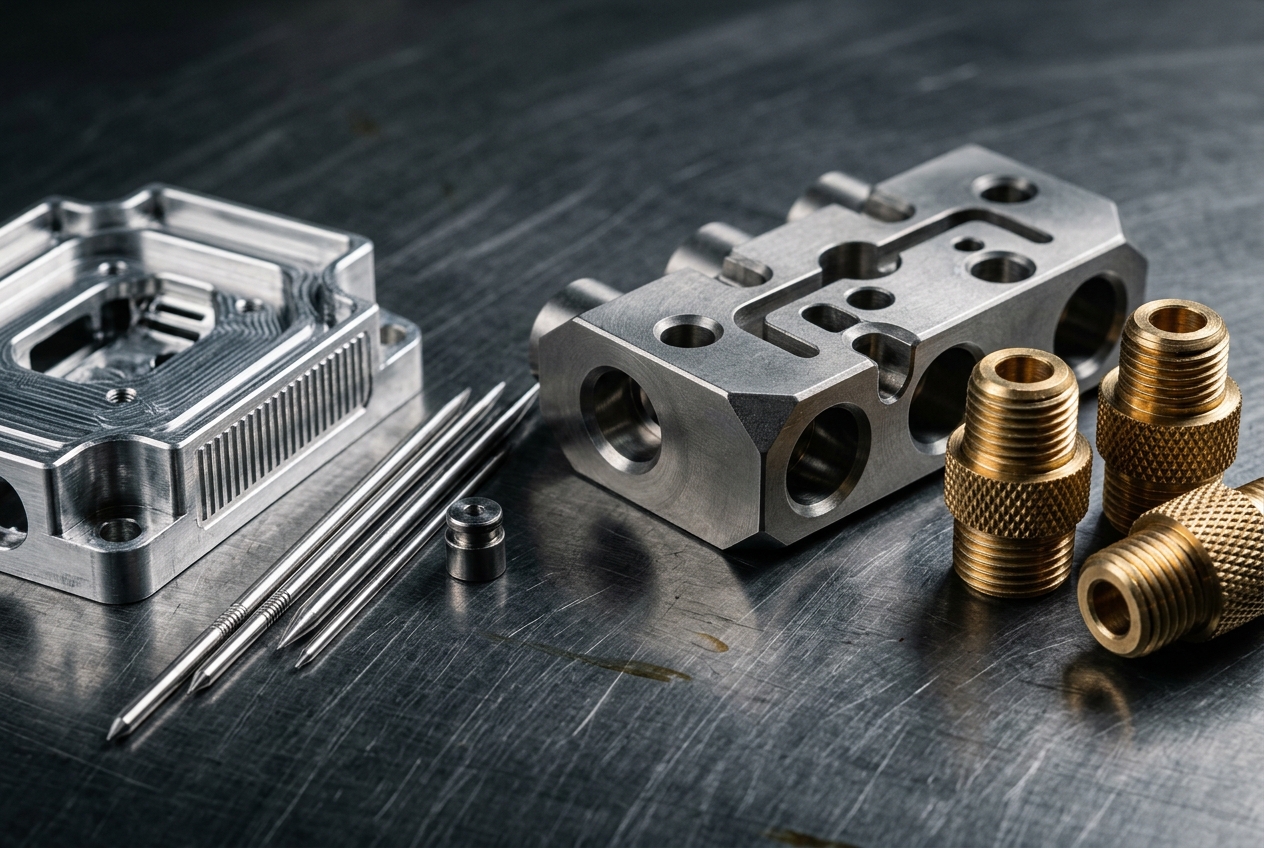
3, 4 and 5-axis CNC milling
Simultaneous 5-axis machining cuts complex geometry, undercuts and impellers in a single setup, which removes stack-up error and handling time. Pallet pools and robotic loading keep spindles running through nights and weekends.
- Axes
- 3, 4, 5 (simultaneous)
- Max envelope
- 40 x 26 x 24 in
- Typical tolerance
- ±0.0002 in
- Surface finish
- to 16 Ra
- Volume
- 1 to 50,000 pieces
- Automation
- Pallet and robot cells
Common parts: structural brackets, manifolds, housings, impellers, fixtures.
CNC turning with live tooling
Turning centers with live tooling, C-axis and sub-spindles finish parts complete, milled flats and cross holes included. Bar feeders support lights-out runs on repeat production.
- Max swing
- 20 in diameter
- Bar capacity
- to 3.25 in
- Typical tolerance
- ±0.0005 in
- Surface finish
- to 16 Ra
- Features
- Live tools, sub-spindle
- Automation
- Bar feed, part catcher
Common parts: shafts, fittings, valve bodies, spacers, threaded components.
Swiss-type screw machining
Sliding-headstock lathes with guide bushings support long, slender, small-diameter parts without deflection. A natural fit for bone screws, pins, probes and micro connectors.
- Bar capacity
- 0.020 to 1.26 in
- Max length
- 12 in per part
- Typical tolerance
- ±0.0002 in
- Surface finish
- to 8 Ra
- Axes
- Up to 12
- Volume
- 500 to 500,000
Common parts: surgical pins, bone screws, sensor probes, electrical contacts.
Wire and sinker EDM
Electrical discharge machining cuts hardened tool steels, carbide and exotic alloys with sharp internal corners and tight radii that conventional tooling cannot reach.
- Wire EDM travel
- 24 x 16 x 12 in
- Typical tolerance
- ±0.0001 in
- Wire diameter
- 0.004 to 0.012 in
- Surface finish
- to 4 Ra skim cut
- Materials
- Hardened steel, carbide
- Sinker
- Graphite and copper
Common parts: punches, dies, gears, blind pockets, turbine slots.
Surface and cylindrical grinding
Finish grinding delivers flatness, parallelism and mirror finishes that turning and milling alone cannot hold. Often paired with EDM for hardened components.
- Surface grinding
- to 24 x 12 in
- OD grinding
- to 10 in diameter
- Typical tolerance
- ±0.0001 in
- Flatness
- 0.0002 in per 12 in
- Surface finish
- to 4 Ra
- Materials
- Steel, stainless, carbide
Common parts: bearing journals, gauge blocks, sealing faces, precision shafts.
Finishing, assembly and kitting
Fewer vendors means fewer hand-offs. Deburring, bead blasting, laser marking and light assembly happen in house. Heat treat, anodize, passivation and plating run through qualified partners we manage for you.
- In house
- Deburr, blast, laser mark
- Managed
- Anodize, passivate, plate
- Heat treat
- NADCAP-approved partners
- Assembly
- Mechanical sub-assemblies
- Packaging
- Kitting, custom foam, VCI
- Delivery
- Scheduled releases
Common work: turnkey sub-assemblies, cleanroom bagging, serialized kits.